
 Cart is empty
Commercial RO Plants: Reliable Water Solutions for Your Business
Introduction
In today’s competitive landscape, ensuring access to clean and safe drinking water is critical for businesses across various industries. PentaPURE offers a range of high-quality commercial Reverse Osmosis (RO) plants tailored to meet the diverse needs of businesses. In this blog, we’ll explore the capacities of PentaPURE’s commercial RO plants, including the 1500 GPD, 3000 GPD, 6000 GPD, and 12000 GPD models, and discuss how they can benefit your operation.
Understanding Commercial RO Systems
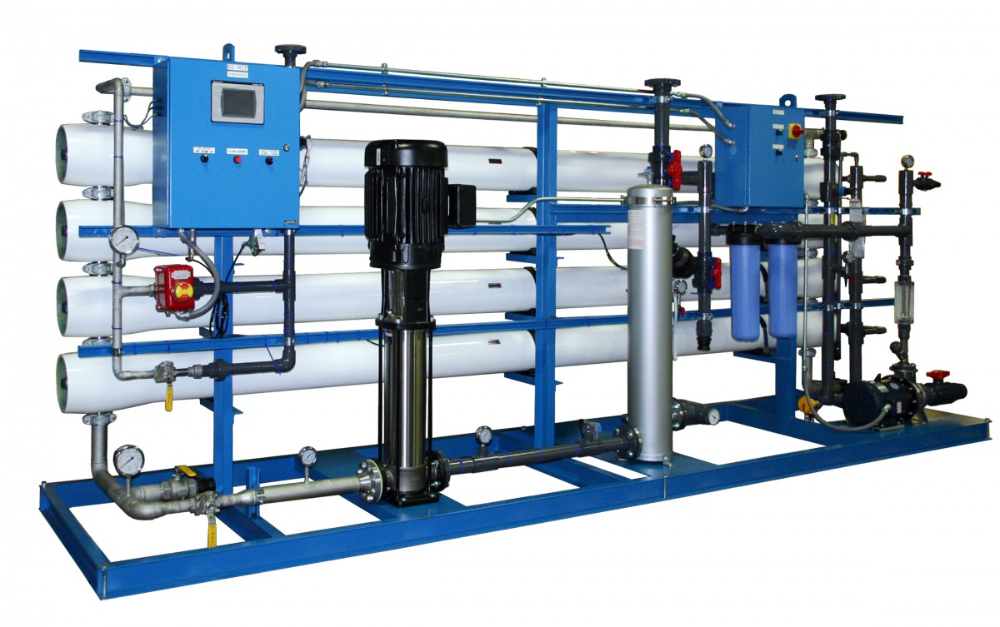
Reverse Osmosis technology effectively removes impurities from water, providing a reliable source of clean water. PentaPURE’s commercial RO plants are designed to handle varying water demands, making them suitable for small businesses to large industrial operations.
1. PentaPure 1500GPD Commercial RO Plant Price in Pakistan
Capacity: 1500 Gallons Per Day (GPD)
Applications: Ideal for medium-sized businesses such as restaurants, schools, and small manufacturing facilities.
Benefits:
- Consistent Water Supply: Perfect for establishments that require a moderate amount of purified water daily.
- Space-Efficient Design: Compact and easy to install, ensuring minimal disruption to your operations.
- High-Quality Filtration: Equipped with advanced filters to remove up to 99% of contaminants, ensuring safe drinking water.
2. 3000GPD Commercial RO Plant Price in Pakistan
Capacity: 3000 GPD
Applications: Suitable for larger businesses such as hotels, hospitals, and larger manufacturing units that need increased water supply.
Benefits:
- Enhanced Capacity: Offers a significant increase in daily water production, meeting the needs of high-demand environments.
- Energy Efficient: Designed to minimize energy consumption while maximizing output, reducing operational costs.
- Robust Performance: Built to handle various water quality inputs, ensuring reliable performance in diverse conditions.
3. PentaPURE 6000 GPD RO Plant Price in Paksitan
Capacity: 6000 GPD
Applications: Tailored for large enterprises, including bottling plants and industrial facilities that require a high volume of purified water.
Benefits:
- Industrial Strength: Engineered to meet the rigorous demands of industrial applications while maintaining optimal water quality.
- Customizable Options: Can be tailored to meet specific operational requirements, including advanced filtration and monitoring systems.
- Durability: Constructed with high-quality materials to ensure longevity and reduce maintenance needs.
4. PentaPURE 12000 GPD RO Plant Price in Pakistan
Capacity: 12000 GPD
Applications: Ideal for very large operations such as factories, large-scale food and beverage companies, and municipal water supply systems.
Benefits:
- Massive Output: Provides a continuous supply of high-quality purified water, essential for large-scale production processes.
- Advanced Technology: Incorporates state-of-the-art technology for optimal performance and efficiency.
- Scalable Solutions: Easily integrates into existing water systems, allowing for future expansion as business needs grow.
Why Choose PentaPURE?
- Quality Assurance: PentaPURE is committed to delivering reliable and effective water purification solutions.
- Expert Support: Our team of professionals is available to assist with installation, maintenance, and any queries you may have.
- Custom Solutions: We understand that every business is unique, and we offer tailored solutions to meet specific requirements.
Conclusion
PentaPURE’s range of commercial RO plants, from 1500 GPD to 12000 GPD, ensures that businesses of all sizes can access safe, clean drinking water. By investing in a PentaPURE RO system, you’re not just ensuring compliance with health regulations but also enhancing operational efficiency and customer satisfaction.
Contact us today to learn more about our commercial RO plants and find the perfect solution for your business needs!

Add a Comment